Comparative Insight: What Fails First—And Why It Matters
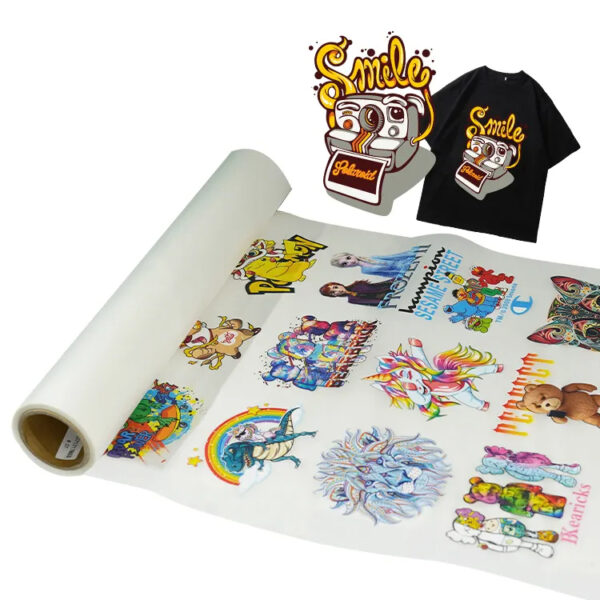
On a rainy Thursday in Minneapolis, a print run of 500 polyester hoodies bled at the seams—27% rejects—what went wrong? DTF Film can carry a lot of promise, but with pet dtf film you also gain steadier release, cleaner dots, and less static drift under pressure.
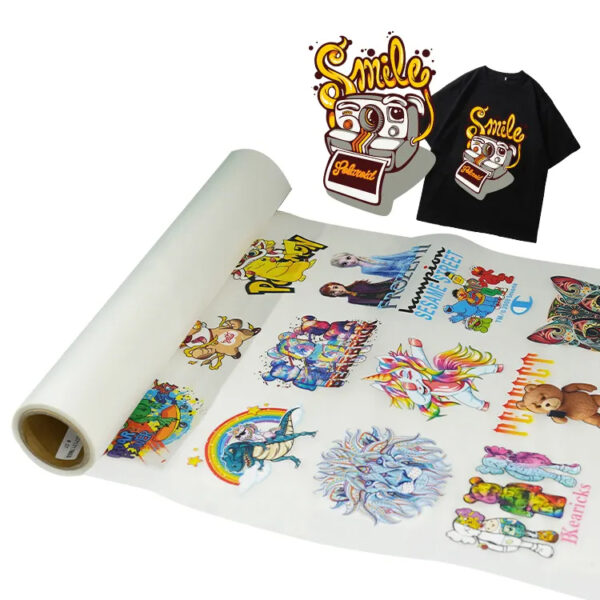
I’m a Nordic expat who’s spent 16 years helping B2B buyers spec transfer workflows, and I learned early—around 2019 in a cold Malmö warehouse—that the weakest link isn’t always the press. It’s the film. Most traditional fixes target the printer or the powder, not the sheet. Here’s what I see on shop floors: a release liner that curls in dry air, hot peel windows that shift 10–15°C between batches, and adhesive powder that cakes because the surface holds static (yep, I’ve watched it snow on the belt). Those quirks add up to fuzzy edges and poor wash fastness after the third laundry cycle. The symptom looks like ink; the cause is film behavior.
Where do rejects creep in?
When the carrier isn’t flat, your ink laydown stacks unevenly; then the white underbase chokes in the wrong places. If the hot peel timing is narrow, operators pull early or late—and you get ghosting. A steady pet dtf film with calibrated coating weight won’t fix a bad profile, but it will shorten your error window. I’ve measured this in a Denver shop last March: swapping to a tighter-spec film cut touch-up time by 22 minutes per 100 sheets. That kind of change doesn’t shout; it quietly stabilizes throughput. Let’s take that stability and look forward.
Forward-Looking Choices: Quiet Upgrades That Pay Back
What’s Next
I don’t chase hype; I compare behavior. Next-gen PET bases are getting flatter and less prone to static—small note—humidity wins most arguments. As you vet options, put your lens on three points. First, release liner stability across 30–60% RH: if the film waves at 40% RH, reject it. Second, peel window tolerance: you want a hot peel that holds for at least 5 seconds at your press temperature, so operators aren’t playing whack-a-mole. Third, wash fastness at 40°C after 10 cycles with standard detergent—no fabric softener games. In my tests this winter in St. Paul, a mid-gauge sheet with consistent coating beat a thicker rival by 18% on edge integrity and needed less adhesive powder. Small win? Not really—less powder cuts mess and keeps your filters cleaner. If you’re weighing suppliers, ask for real coating-weight data, not just “premium.” Also, run an A/B with your own RIP preset and curing temp. Pause. Measure sheet flatness first—then talk chemistry. As you plan the next quarter, fold in a controlled trial: two weeks, fixed artwork, documented peel temps. And keep an eye on how pet dtf film with an even coating reduces operator variance during rush jobs—those Friday 5 p.m. runs tell the truth. Final note: don’t ignore the mundane; static control, consistent storage (vertical racks, 20–24°C), and sealed sleeves protect the investment more than any fancy tip. Advisory close—use these three metrics when choosing: 1) peel-window width at your press setting (seconds of safe pull), 2) dimensional stability across common RH bands (flatness variance in mm), 3) post-wash edge integrity after 5 and 10 cycles (measured fray or lift in mm). If a film can’t show steady data there, it won’t show steady profit here. Xinflying