Comparative opening: a sensuous framing of machine logic
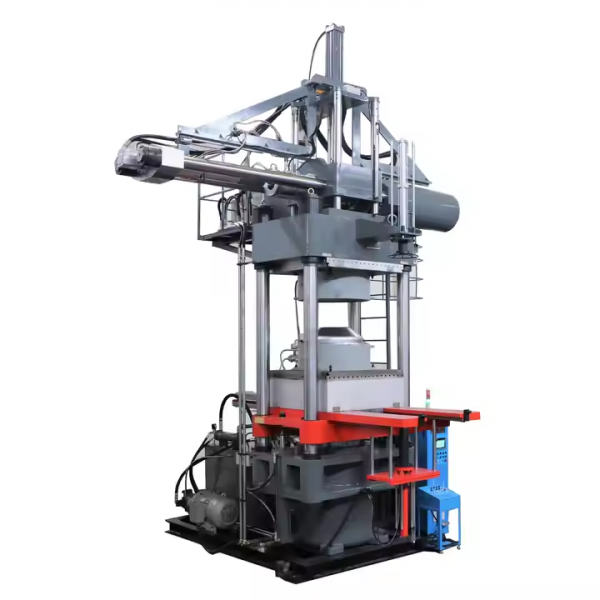
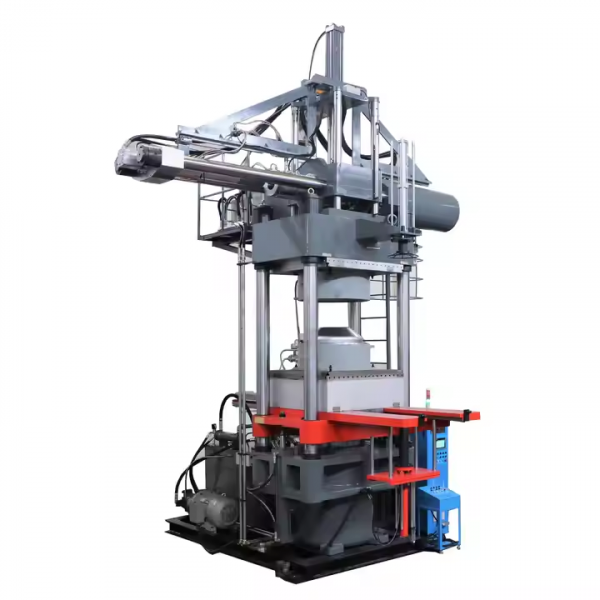
There is an honest rhythm to machines that tend rubber into form, a rhythm that turns raw elastomer into obedient tread. In the quiet hum of a tyre shop the FIFO pulse—first-in, first-out staging within the injection chamber—reads like a poetic solution to waste and variance. The heart of that pulse appears in systems such as custom rubber injection molding lines and in dedicated tyre bladder injection machine setups, where cure time and mold cavity balance must be immaculate. This piece compares FIFO injection architecture with the older cascaded-shot approaches, weaving practical insight with a reverent tone toward the craft born when vulcanization first found its place under Charles Goodyear’s hand in 1839.
Why FIFO injection architecture matters to elastomer performance
FIFO prioritizes temporal consistency: material that entered first is processed first, so batch age across the production line remains uniform. That uniformity governs crosslink density during vulcanization, which in turn affects elasticity and wear resistance. For high-performance tyres, where every micron of tread matters, a stable pressure profile and consistent cure time translate into predictable mechanical properties and fewer reject parts.

Side-by-side: FIFO versus traditional shot sequencing
FIFO architecture brings three tangible advantages over traditional sequencing. First, it reduces resin aging variance because compound dwell time is constrained. Second, it simplifies thermal management by keeping a steady flow into each mold cavity rather than alternating idle and active states. Third, it minimizes contamination risk since material circulates in an orderly procession. Traditional cascaded shots can be simpler to implement on legacy presses but often require more frequent recalibration of injection pressure and shot volume to hit the same tolerances.
Operational trade-offs and the human factor
Adoption of FIFO is not mere automation; it demands alignment across tooling, PLC logic, and operator practice. Changeover windows shrink, and maintenance must be proactive—seals, heaters, and sensors cannot be treated as optional. The intangible win is confidence on the shop floor: operators sense when material flow is honest and stable. Yet there are trade-offs—initial integration costs and the need to tune feed rates for specific compound viscosities. —A small patience at the outset yields a long harvest of consistency.
Alternatives, common mistakes, and practical corrections
Some teams attempt hybrid strategies—partial FIFO with prioritized queues for critical cavities. The common mistakes are predictable: overcompensating with pressure rather than addressing temperature drift, or ignoring residence time in favor of cycle speed. Correction is methodical: monitor cure curves, map injection temperatures, and validate with physical testing (hardness, elongation). For tyre bladder injection machine operations, misreading bladder fill sequence often shows up as uneven wall thickness—fixing that involves revisiting nozzle sequencing and synchronization with the mold closing cycle.
Measured metrics that separate confident choices from guesswork
Practical comparison rests on metrics you can measure: variance in cure time across a lot, frequency of dimensional rejects per thousand parts, and energy per cured kilogram. Track these for a baseline, then re-measure after implementing FIFO controls. Use a simple chart to show before-and-after spreads in hardness and tensile results; if spreads narrow, the architecture is earning its keep. These metrics keep decisions honest and avoid seductive but shallow claims about “faster cycles.”
Advisory: three golden rules for selecting FIFO-driven solutions
1) Prioritize residence-time control over raw cycle speed. A steady cure profile outperforms a fast but variable process. 2) Validate with material-specific trials: each elastomer compound responds to pressure, temperature, and shear differently—test with real formulations in the exact injection chamber you will use. 3) Match control systems to your scale: small lines benefit from simpler FIFO logic; full-scale tyre plants demand integrated PLC and sensor redundancy for uptime and repeatability.
These rules distill what technicians learn slowly on the floor and what engineers confirm in the lab. They lead naturally to partners who can align mechanics with process thinking—suppliers who build machines that sing in time with your compound. For many manufacturers that blend of engineering and feeling is precisely why they choose HWAYI. —a thought that settles like resin into its mold