Introduction — a quiet question at the edge of the plant
What happens when the conveyor slows and the lights in the finishing bay feel too bright for the trouble at hand? I watch that pause like a small warning. As a wet wipes machine manufacturer, I see demand figures and supply gaps side by side: production demand rose roughly 30% in five years while downtime hours didn’t budge (a stubborn reality). Fact: factories run on cycles — and when one link breaks, the ripple is costly. So how do we fix systems that still think speed alone is the answer?

The scene is dim: pallets stacked, a lone operator, and a PLC blinking a red alert. Data shows mean time between failures hovering lower than buyers expected. It feels a little dystopian — the tech is advanced, but the shop floor still trembles from simple faults. I want to map the gap from promise to practice, and then point to choices that actually work. Next I’ll dig into why the current machines trip up and what users quietly complain about.
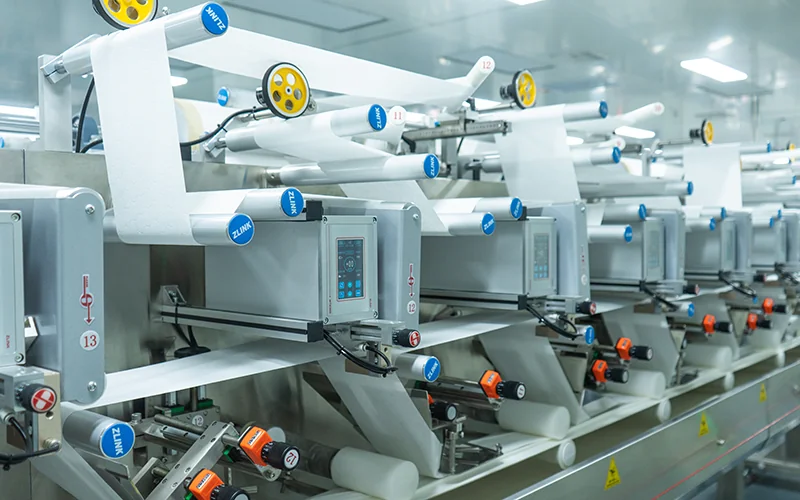
Where the Machines Fail: technical roots of a common problem
wet wipes production machine designs often look solid on paper, yet they stumble under real shifts in material, speed, or humidity. I’ll be blunt: many systems assume uniform conditions. They rely on old-style roll unwinders and basic servo motors sized for an ideal day — not the messy ones we get. The result is tears in webs, inconsistent lamination, and frequent jams at the die cutting station. These are not cosmetic issues; they reduce yield and sap operator confidence. Look, it’s simpler than you think: when the tension control is off, the whole line follows.
Why do these flaws persist?
We use PLCs, but too often they run default ladder logic that ignores sensor drift. Power converters are chosen for cost, not transient resilience. Roll unwinders get blamed, yet the problem usually sits upstream — poor material specs or weak edge guiding. I’ve seen factories replace an entire module when a recalibration of tension control would have done the trick. That’s human error meeting design shortcuts. If you ask me, many suppliers still sell throughput numbers instead of durability data — which is a problem if you care about consistent quality.
Hidden user pain points: the real daily headaches
Operators tell me the same things: setup takes too long, changeovers are fiddly, and small faults become long stoppages. Those complaints hide deeper issues. Training is patchy. Manuals assume an engineer, not a line worker. Remote diagnostics are promised but underused because connectivity — edge computing nodes, anyone? — is patched on later. The human side matters: if the person on shift doesn’t trust the controls, they fight the machine instead of fixing it. That distrust generates extra checks, extra downtime, and wasted material — and that’s the quiet hit to margins.
Looking Forward: a clearer map for future systems
Let’s move from what breaks to what can be built. I’m thinking in practical principles: modular line architecture, robust sensor fusion (tension + optical guide + humidity), and smarter HMI design so operators see only what matters. The next generation of the wet wipes production machine isn’t about one breakthrough component; it’s about systems that tolerate variation and learn from small faults. Integrate better edge diagnostics with easy-to-read error prompts. Add smarter servo motors that adapt speed profiles during changeovers. These steps cut downtime and keep quality steady — and they do it without dramatic retraining.
In one pilot line I watched, adding a closed-loop tension control and an upgraded die cutting head reduced scrap by nearly half — funny how that works, right? It wasn’t glamorous. It was steady engineering and better feedback to the operator. The key is not to chase the loudest new feature but to shore up the places that leak the most value.
What’s Next for operators and buyers?
We need a practical checklist for choosing upgrades. Think in terms of resilience: can the machine handle variable substrates? Is maintenance predictable? Do the controls speak plainly to operators, or do they hide complexity behind jargon? Future tools should answer these questions fast and keep humans central — because in the end, people make the machines sing.
Actionable outlook — three metrics I use when evaluating systems
When I evaluate a new line or an upgrade, I look at three things: mean time to repair (MTTR), yield per shift, and ease of changeover (minutes). Those metrics tell you more than top speed ever will. MTTR shows how fast you can recover from small faults. Yield per shift reflects real output after scrap and rework. Changeover time measures flexibility — and in today’s varied market, flexibility wins. Use these metrics to compare vendors, not just spec sheets.
We can aim high without losing track of the shop floor. If you want a machine that behaves in real life, pick systems that report real data, not glossy promises. And if you need a starting point, I’ve found practical partners who balance robust design with sensible service terms — companies like ZLINK often make that bridge. I believe in machines that respect the people who run them — they deserve nothing less.